Main menu Open search

Blog

2026 Top Solvent Free Lamination Machine Types?

In 2026, Solvent Free Lamination is moving from a specialist option toward a mainstream packaging investment. Smithers’ report, The Future of Flexible Packaging to 2028, identifies sustainability, downgauging, and production efficiency as major market drivers. Grand View Research also reports steady growth across flexible packaging, supported by food, medical, and consumer applications.

The machine choice now matters more than a simple speed comparison. Two-component polyurethane systems remain common for standard film structures. High-speed duplex machines suit large snack and pouch volumes. Triplex lines support complex barriers, such as PET, aluminum foil, and PE combinations. Compact models can help converters reduce floor space and trial new substrates. These are practical differences, not marketing labels.

“No machine wins every job.”

Nordmeccanica president Pier Luigi De Rossi has described the principle this way: “Solventless lamination is a process, not simply a machine purchase.” His comment reflects a critical reality. Adhesive viscosity, coating weight, nip pressure, curing time, and operator experience can change results dramatically. A fast line may still produce weak bonds or visible tunnel defects when materials are poorly matched.

This 2026 guide will compare major Solvent Free Lamination Machine Types by structure, output, automation, and application. It will also examine energy use, waste control, maintenance, and return on investment. Some assumptions deserve scrutiny. The newest machine is not always the most suitable one. Performance begins with the packaging structure, not the brochure.
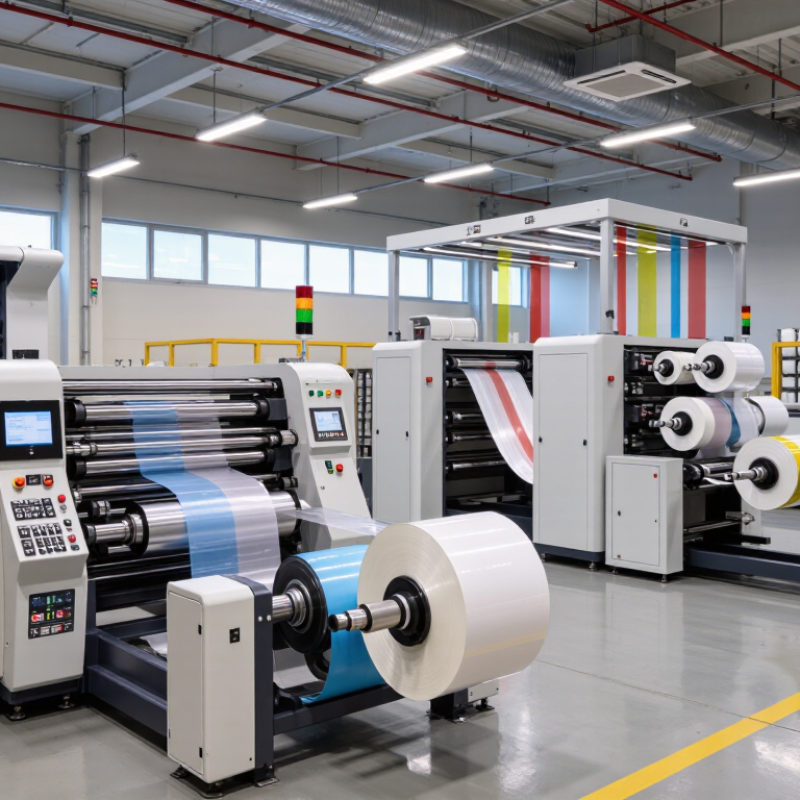
2026 Top Solvent Free Lamination Machine Types?

What Is Solvent-Free Lamination? 0% Solvent and 0.8–2.5 g/m² Adhesive

2026 Top Solvent Free Lamination Machine Types?

Solvent-free lamination uses no evaporation solvent. A two-component polyurethane adhesive is mixed, metered, and applied directly between films. Typical adhesive consumption ranges from 0.8 to 2.5 g/m², depending on film surface, bond strength, and application speed. There is no drying oven. That reduces heat exposure and simplifies the production line.

The main machine types include single-station duplex laminators, tandem laminators, and coating systems with precision metering rolls. Duplex models suit common film-to-film work. Tandem systems support higher output and multiple-layer structures.

A stable mixing ratio matters more than impressive speed. Even a small error can create weak bonds, bubbles, or uneven curing.

Smithers’ report, The Future of Flexible Packaging to 2028, forecasts continued growth in flexible packaging demand, increasing pressure for efficient coating and lamination equipment.

Technical guidance from FEICA also highlights accurate adhesive dosing, substrate cleanliness, and controlled curing as essential process factors. In practical operation, web tension and nip pressure must remain steady across the roll. The target is precise.

Solvent-free does not mean maintenance-free.

Mixing heads need disciplined cleaning, and operators must verify coat weight with regular measurements. The 0.8–2.5 g/m² range is useful, but not universal. A thinner adhesive layer may fail on a difficult substrate, while excessive coating wastes material and extends curing time. That balance still requires testing.

How Do 2K PUR Laminators Work at 40–80°C and 100–500 m/min?

2026 Top Solvent Free Lamination Machine Types?

A 2K PUR laminator combines two reactive polyurethane components shortly before coating. A metering unit controls their ratio, while a static mixer creates a uniform adhesive. The mixed adhesive passes through a heated coating head, commonly operating between 40 and 80°C. Heat lowers viscosity and supports a stable, thin coating. It does not remove solvent, because the process is solvent free.

The web then enters a controlled laminating nip. Pressure joins the coated film with paper, foil, or another polymer layer. At 100–500 m/min, tension control becomes critical. Small web movement can create wrinkles, telescoping, or uneven bonding. Operators monitor coating weight, nip pressure, roller temperature, and component flow continuously. Faster production also leaves less time to correct defects.

A practical lesson from line trials is simple: speed cannot replace accurate dosing. A minor ratio error may cause weak bonds, surface marks, or incomplete curing. Ambient moisture also affects the final reaction. Not every line should run at 500 m/min. That target depends on film structure, adhesive chemistry, machine design, and curing time. Some settings look efficient but become unstable after several hours. Careful operators record those changes, question the data, and adjust temperature gradually rather than forcing the highest speed.

Which Machine Types Support 300–2,000 mm Webs and 100–500 m/min?

2026 Top Solvent Free Lamination Machine Types?

For 300–2,000 mm webs, machine selection depends on coating control, tension stability, and adhesive chemistry. Compact two-roll laminators suit narrow and medium webs, often around 300–1,300 mm. They are practical for flexible packaging and shorter production runs. Heated rollers help maintain adhesive flow, especially when ambient temperatures change.

Wide-web lines usually use precision multi-roll coating stations. These machines can support webs near 2,000 mm and speeds from 100 to 300 m/min. A controlled mixing and metering unit reduces coating variation across the web. At higher speeds, tandem or duplex configurations provide better throughput and process flexibility. Some systems can reach 500 m/min, but only with accurate nip pressure, automatic tension control, and reliable curing conditions.

Speed is not the whole story. A 500 m/min line may struggle with lightweight films, trapped air, or uneven adhesive distribution. I have seen specifications look impressive while actual production speeds remained lower. That gap deserves careful testing. Operators should review web thickness, adhesive coat weight, splice handling, and curing time before purchase. Servo-driven unwind and rewind sections improve registration and reduce wrinkles. Wider webs also need stronger frame construction and precise roller alignment. For demanding applications, trial laminations with real substrates reveal more than a brochure. Performance can change significantly after maintenance, so accessible rollers and simple cleaning procedures matter.

How Do 2026 Models Cut Energy Use by 30–50% Versus Solvent Lines?

2026 solvent-free laminators are increasingly built around two-roll, multi-zone, and duplex coating configurations. Their main advantage is simple: they do not evaporate large volumes of solvent. Less heat is needed. This removes the energy demand of long drying ovens, exhaust fans, and solvent recovery equipment. In well-controlled production, total energy use can fall by 30–50% compared with conventional solvent-based lines. The actual result depends on film structure, adhesive coverage, line speed, and factory conditions.

Modern models also reduce waste through servo-driven metering, automatic tension control, and faster recipe changes. Heated coating rollers maintain stable adhesive temperature without warming an entire oven chamber. Insulated zones limit heat loss during operation. Smart standby functions lower power when the web stops.

A realistic energy audit should measure electricity, thermal oil, compressed air, and ventilation separately. Otherwise, the saving may look better than it is.

From a production perspective, accurate gap control matters as much as machine size. Uneven adhesive weight can create bubbles, wrinkles, or rework, which quietly increases energy consumption. Operators should verify bond strength after curing, not judge quality from appearance alone.

Some factories report savings near 50%, but that figure is not universal. A poorly tuned solvent-free line may consume more power than expected. This is the part many comparisons miss. Reliable evaluation needs several weeks of measured data, including start-up losses, cleaning time, and rejected rolls.

How Should Buyers Compare 2–6 g/m² Coat Weight and ±1% Tolerance?

2026 Top Solvent Free Lamination Machine Types?

Solvent-free laminators commonly use two-component reactive adhesives, with two-roll, multi-roll, or precision slot-die coating systems. Buyers should compare more than machine speed. The coating unit must maintain stable adhesive mixing, temperature, viscosity, and web tension. Small changes can create visible streaks, weak bonds, or excessive squeeze-out.

For a stated coat weight of 2–6 g/m², clarify what ±1% means. At 2 g/m², a true ±1% tolerance allows only 1.98–2.02 g/m². At 6 g/m², the range becomes 5.94–6.06 g/m². That is extremely narrow. Some suppliers may mean ±1 g/m² instead, which is very different. Ask for test data across the full web width, not only the center. Confirm the measurement method, sampling frequency, adhesive temperature, line speed, and substrate combination. A perfect number on a brochure is not proof.

Tips: Request a production trial using your actual film structure. Check coating uniformity after curing, not only immediately after lamination. Review gravimetric or optical measurements from both edges and the center. Also inspect splice areas and speed changes. In my experience, operators often blame the metering roll first, while unstable adhesive temperature causes the real drift. Still, this is not universal. Verify it.

Exclusive Access

Unlimited Resources

Detailed information on our products to assist you with the planning of your cable management project

Register Now

BIM Files

Step Files

Installation Manuals

User Guides

Best Practice Guides

Technical Charts